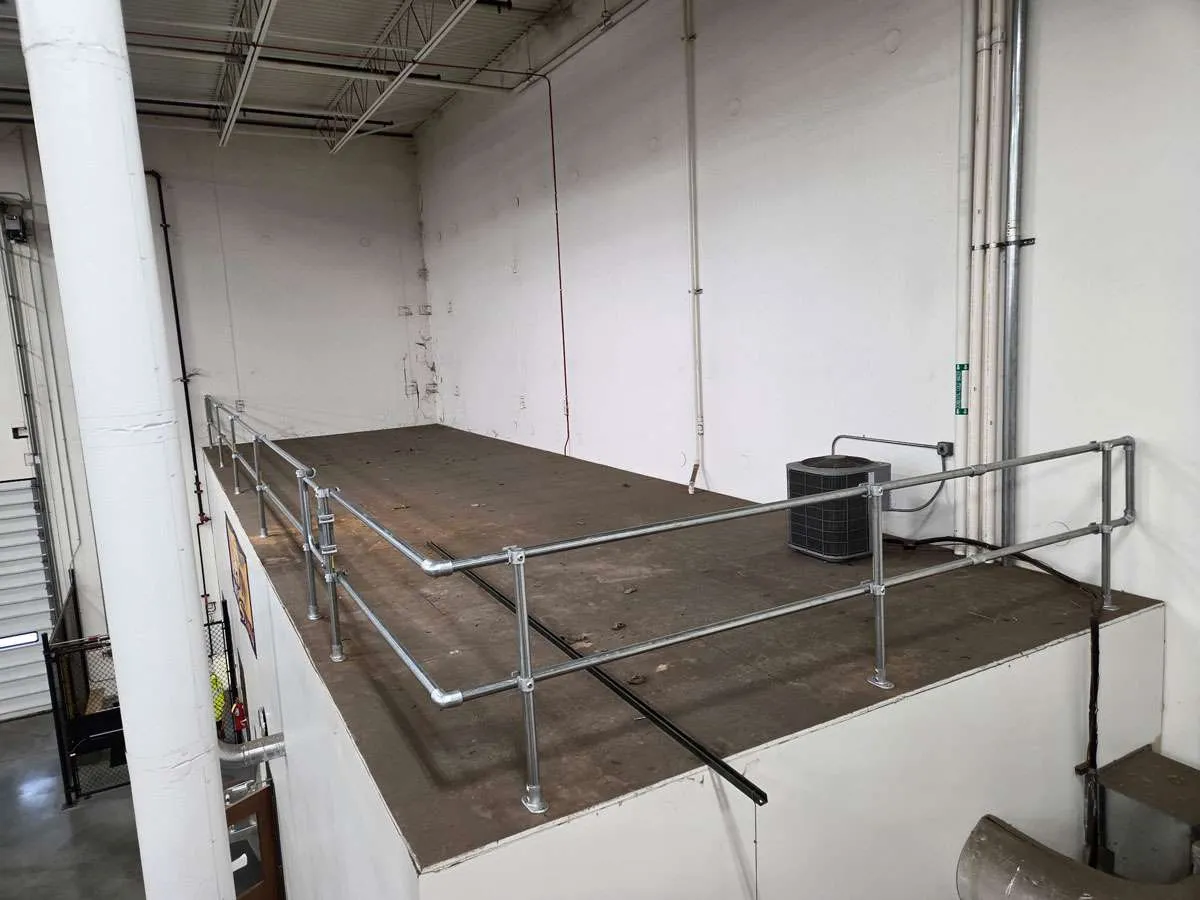
Project Overview
Industry: Industrial Gas Distribution
Location: Midwest Distribution Center
Products Installed: Modular Guardrail System, Self-Closing Safety Gates, Access Ladders
Project Snapshot
- Industry: Industrial Gas Distribution
- Challenge: Protect maintenance personnel working on elevated mezzanines while maintaining access to conveyors and equipment
- Solution: Modular OSHA-compliant guardrail system with safety gates and fixed access ladders
- Benefits: Improved worker safety, minimal facility modifications, faster installation, uninterrupted operations
Overview
Distribution centers often require maintenance personnel to access conveyors, mechanical equipment, and elevated work areas located on mezzanines. Without proper fall protection, these routine maintenance tasks can expose workers to serious fall hazards and create OSHA compliance concerns.
A leading industrial gas distributor partnered with Lighthouse Safety to improve safety around elevated maintenance areas while preserving existing operations. Using a modular guardrail solution, Lighthouse Safety created a customized system that protected employees, simplified installation, and minimized disruption to the facility.

The Challenge

The customer’s distribution center relied on elevated mezzanines that housed conveyors and mechanical equipment requiring regular maintenance.
Technicians needed safe access to these areas for inspections, repairs, and preventative maintenance. However, the existing layout created several challenges:
- Employees were exposed to fall hazards while servicing elevated equipment.
- Existing conveyors and machinery limited where traditional guardrail systems could be installed.
- The customer wanted to avoid expensive structural modifications.
- Operations needed to continue with minimal downtime during installation.
The facility required an OSHA-compliant fall protection solution that could be customized around existing equipment without interrupting daily operations.
The Solution
After receiving an inquiry through its website, Lighthouse Safety followed a consultative process to design a solution tailored to the facility.
The project included:
- Initial consultation to understand maintenance activities and fall hazards
- On-site facility assessment with measurements and photographs
- Evaluation of equipment locations and maintenance access points
- Collaborative review of recommended solutions
- Final installation of a customized modular fall protection system


The completed solution combined:
- Modular Guardrail System
- Self-Closing Safety Gates
- Fixed Access Ladders
Because the guardrail system uses a modular tube-and-fitting design, Lighthouse Safety was able to install guardrails around existing conveyors and mechanical equipment without requiring significant structural modifications or relocating equipment.
This approach allowed the customer to improve safety while maintaining normal facility operations throughout the installation.
Why a Modular Guardrail System?
Traditional welded guardrail systems often require extensive fabrication or modifications to existing structures.
A modular safety railing offered several advantages for this project:
- Adapted around existing conveyors and equipment
- Required little to no structural modifications
- Faster installation than custom-fabricated alternatives
- Durable galvanized steel construction
- Easy to expand or reconfigure as facility needs change
- Continuous passive fall protection without relying on personal fall arrest equipment

For facilities with changing layouts or complex equipment configurations, modular safety railing systems provide a flexible long-term safety solution.
Benefits
The completed system delivered both immediate and long-term benefits for the customer.
Improved Worker Safety
Maintenance personnel now have protected access to elevated work areas, reducing exposure to fall hazards during routine inspections and repairs.
OSHA Compliance
The new guardrail system helps support OSHA walking-working surface requirements by providing passive fall protection around elevated maintenance areas.
Minimal Facility Disruption
Because the modular guardrail system fit around existing equipment, installation was completed without major facility modifications or extended downtime.
Flexible Design
The tube-and-fitting construction allows future modifications or expansion if equipment layouts change.
Faster Installation
The modular design reduced installation complexity compared to engineered fall arrest systems or custom-fabricated guardrails.
Products Used
This project incorporated several complementary fall protection products to create a complete access solution.
Modular Guardrail System
A permanent modular guardrail system that provides passive fall protection around elevated work areas while adapting to existing facility layouts.
Self-Closing Safety Gates
Installed at ladder openings and access points to maintain continuous fall protection whenever personnel enter or exit elevated areas.
Fixed Access Ladders
Provided safe, reliable access to mezzanines and elevated maintenance locations.
Results

Lighthouse Safety successfully delivered a customized fall protection solution that improved worker safety while preserving the customer’s existing infrastructure.
The modular guardrail system eliminated the need for extensive structural modifications and provided maintenance personnel with safer access to elevated equipment.
By combining modular guardrail systems, self-closing safety gates and fixed access ladder products into one integrated solution, Lighthouse Safety helped the customer improve OSHA compliance, reduce installation complexity, and create a safer maintenance environment without disrupting daily operations.
Frequently Asked Questions
Why are guardrails important for mezzanine safety?
Guardrails provide passive fall protection by creating a physical barrier that helps prevent falls from elevated work areas. Unlike personal fall arrest systems, guardrails protect workers continuously without requiring specialized equipment or user action.
Can modular guardrails be installed around existing equipment?
Yes. Modular guardrail systems like Kee Guard are designed to adapt around existing conveyors, machinery, and structural obstacles, making them an ideal solution for retrofit projects.
What OSHA regulations apply to mezzanine fall protection?
OSHA requires employers to protect workers exposed to fall hazards on walking-working surfaces. Properly designed guardrail systems can help facilities meet applicable OSHA requirements for elevated work areas.
Why choose passive fall protection instead of personal fall arrest systems?
Passive fall protection systems, such as guardrails, protect every worker automatically. They require no harnesses, anchors, or user training before each task, making them one of the most effective and reliable methods of fall prevention for many maintenance applications.
Need a Custom Fall Protection Solution?
Every facility presents unique fall hazards. Lighthouse Safety designs customized guardrail systems, safety gates, access ladders, and complete fall protection solutions for distribution centers, warehouses, manufacturing facilities, and industrial operations throughout North America.
Contact Lighthouse Safety today to schedule a facility assessment and discover how a customized fall protection solution can improve worker safety while supporting OSHA compliance.